Customized Evaporation, Concentration, and Distillation Solutions: Reshaping the Green Engine of Industrial Separation and Resource Recycling
In the era of industrial green transformation and cost reduction and efficiency improvement, we focus on providing high-energy-consuming and high-emission enterprises with one-stop customized solutions of "evaporation concentration + distillation purification".
Customized Evaporation, Concentration, and Distillation Solutions: Reshaping the Green Engine of Industrial Separation and Resource Recycling
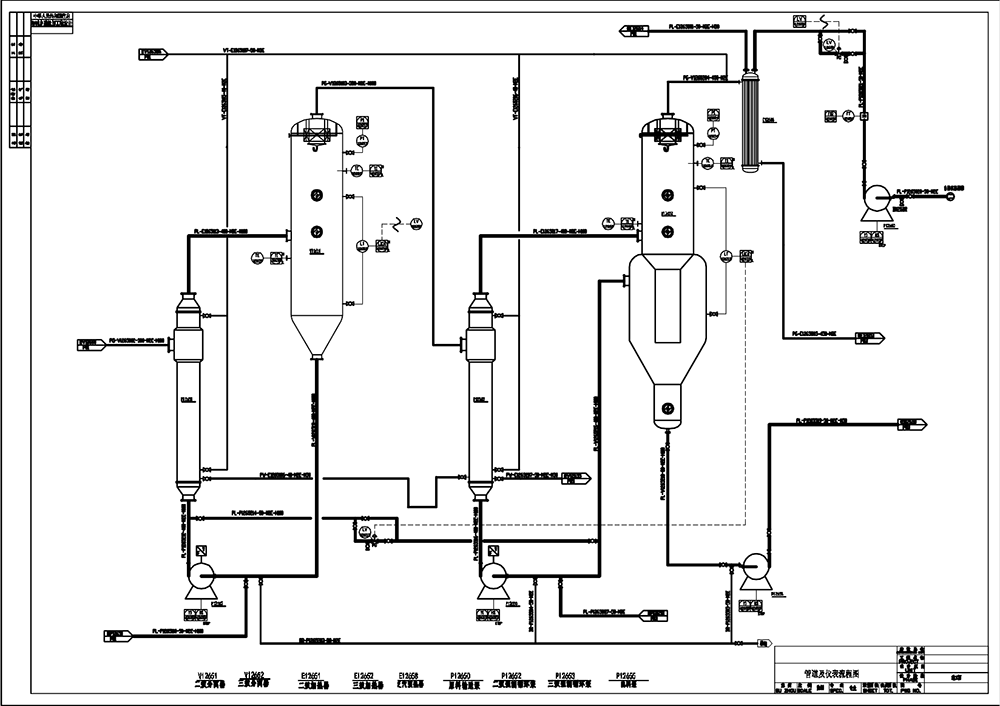
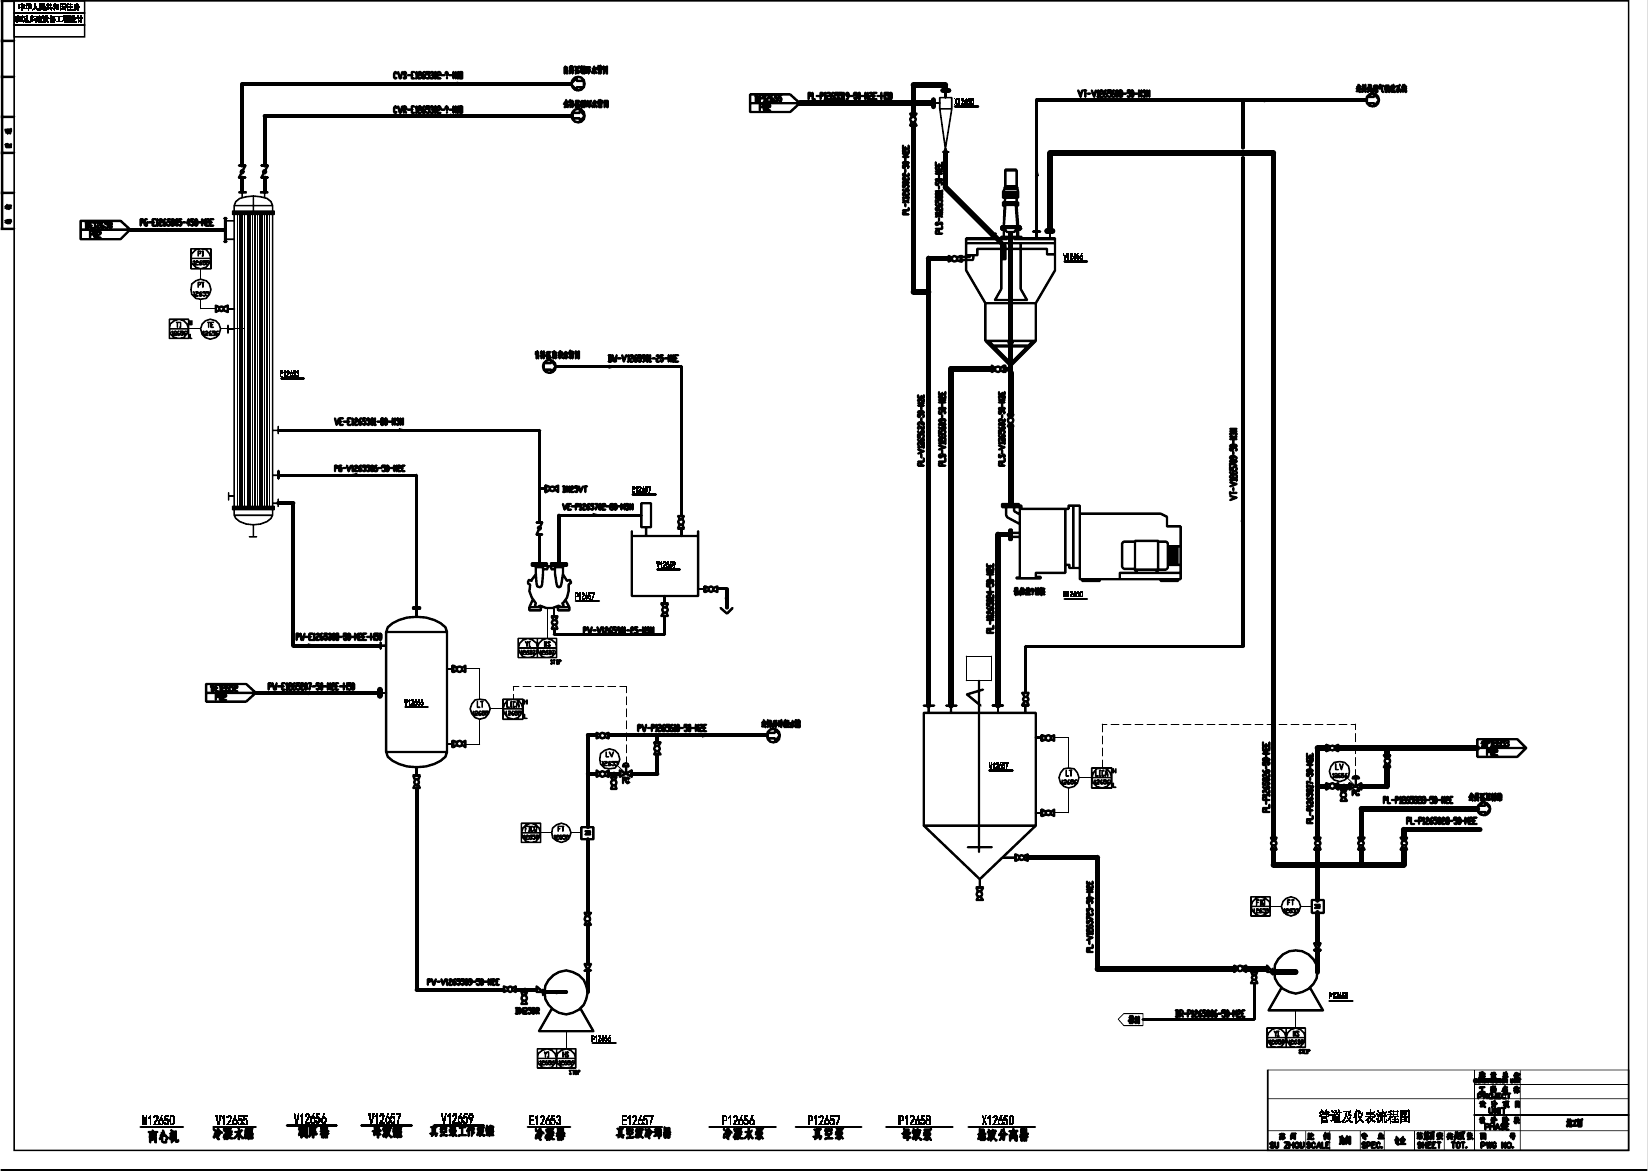
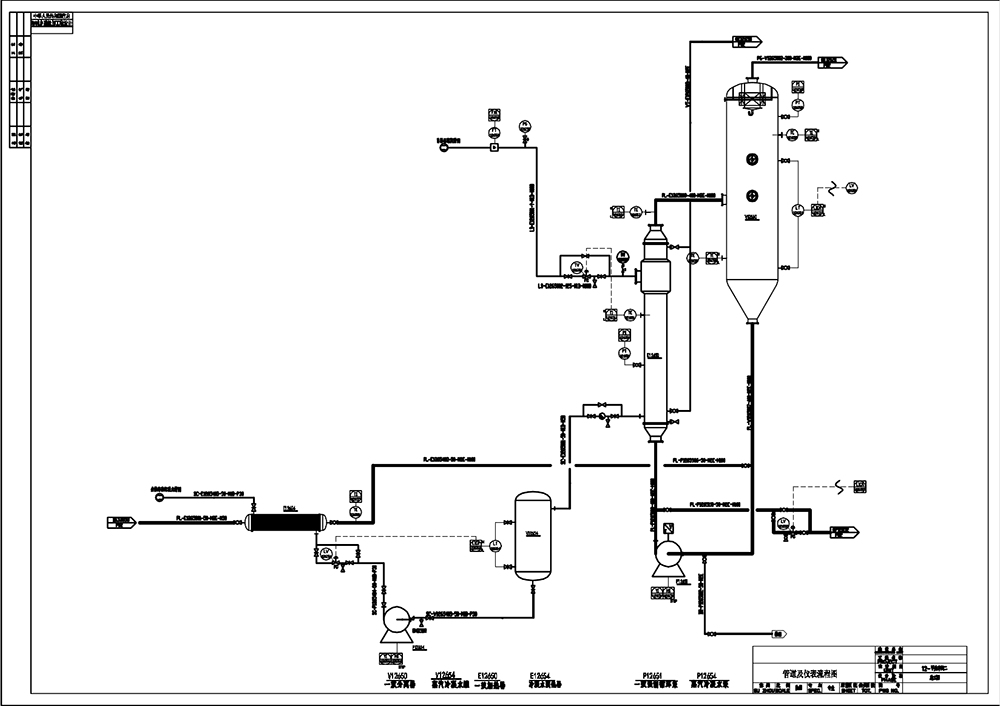
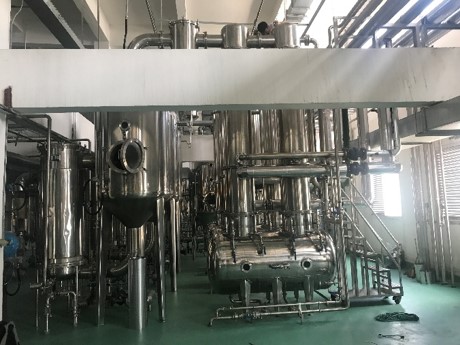
We reject standardized, one-size-fits-all equipment. Instead, relying on our profound thermodynamics expertise and rich engineering experience, we deeply analyze your material characteristics and process pain points to tailor a complete separation and purification system for you, from laboratory pilot testing to industrial mass production, transforming every drop of waste liquid into high-value-added resources. Core Technology Matrix and Process Advantages Our customized solutions deeply integrate cutting-edge energy-saving separation technologies, achieving breakthroughs in both energy efficiency and purity through multi-process coupling: MVR and Heat Pump Distillation Coupling Technology: Precision Salt Separation and Crystallization Separation Technology: Full-Scenario Customized Service Capabilities Our solutions possess strong material adaptability and process inclusiveness, broadly empowering major core industries: Waste acid and alkali recovery and solvent recycling: Fine chemicals and new energy materials: Food Fermentation and Environmentally Friendly Zero Emissions: Full Lifecycle Turnkey Service. From concept to implementation, we provide comprehensive, end-to-end services. In the early stages, a team of senior experts conducts water quality analysis, process simulation, and pilot-scale verification to ensure the solution is flawless. In the mid-stage, relying on a modern manufacturing base, we achieve precision machining and modular assembly of equipment. In the later stages, we provide on-site installation and commissioning, personnel training, and 24/7 intelligent remote operation and maintenance monitoring. We not only deliver a set of highly efficient separation equipment, but also dedicate ourselves to building a low-carbon, circular, and high-yield modern production line for you.